Hey everyone, it’s Jake here, and if you’ve ever bought carbon steel from me (or even just googled “how to make steel last longer”), you’ve probably heard the word “tempering” thrown around. I get it—for a second, I used to mix it up with quenching, and I’ve had customers ask me at trade shows if it’s a type of spicy sauce (side note: it’s not, though I get the appeal). Today we’re breaking this down real simple, no stuffy metallurgy jargon, just the straight scoop on what tempering is, why it matters, and how it’s the reason so many of the carbon steel products I supply hold up when you need them to. Carbon Steel
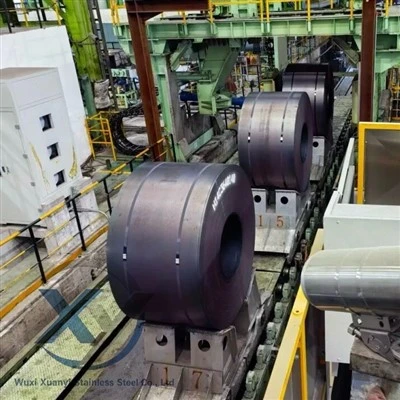
First, let’s do a quick reset on how carbon steel gets hard, because you can’t understand tempering without that. When we make most carbon steel parts, the first big step is quenching. That’s when you heat the steel up to like 1500–1600°F (way hotter than your kitchen oven, trust me) and then dunk it super fast in water, oil, or even polymer. That quick cool-down locks the steel’s internal structure into something called martensite—think of it as a super tight, brittle grid, like a pile of toothpicks crammed so tight you can barely bend it, but also it will snap if you nudge it too hard. Quenching makes steel hard as hell, but it’s way too fragile for 90% of the stuff we use carbon steel for: drill bits, bolts, truck springs, even the wrenches you keep in your toolbox. Most of those need to flex a little, not shatter if you drop them. That’s where tempering comes in.
Tempering is basically reheating the quenched, brittle martensite steel to a temperature way lower than the original heat-up temp—usually between 400°F and 1300°F, depending on what we need the final part to do—and then cooling it slow (or sometimes even air-cooling, it’s not as strict as quenching). What this does is loosen up that tight martensite grid just enough, rearrange the internal carbon particles so they’re not all crammed in a mess, and get rid of the internal stress quenching left behind. It’s like going from folding a fitted sheet so tight it won’t stay on the bed to folding it neatly so it works as a blanket—still firm, but not impossible to use.
Wait, let’s test that with a real example, because I hate abstract stuff. If I supply a set of wrenches made from 1045 carbon steel, we don’t leave them as-quenched. Quenched 1045 would be so hard it’d chip if you tried to loosen a rusted bolt. But if we temper it at around 800°F, that 1045 becomes hard enough to grip the bolt and tough enough not to crack when you hit the wrench with a hammer (yes, people do that, I’ve seen it). If we tempered it at a lower temp, say 500°F, it’d be way harder but super brittle—maybe great for a pickaxe head, but terrible for wrenches. Temper at 1200°F, and it’d be way too soft, like a paper clip that got left in a campfire too long—bends over if you look at it. So it’s all about picking the right temper temperature for the job.
A lot of people ask me: “Isn’t tempering just making steel less hard?” Eh, sort of, but it’s way more nuanced than that. We tune the hardness and toughness exactly to what the customer needs. Let’s break down some common temper temps and uses, since I deal with this every single day. When I supply leaf springs for semi-trucks, those need to flex thousands of times without breaking—so we temper at around 1000°F. That gives the steel enough give to handle the rough roads, but still enough hardness to support the weight of a full load. For drill bits? We use a lower temper, like 600–700°F. Drill bits need to stay hard enough to bore through metal, but not so brittle they snap halfway through a hole. And for something like a screwdriver blade? Mid-range, around 700–900°F—hard enough to not bend when you’re turning a tight screw, tough enough that if you slip with the screwdriver, it just scuffs, not snaps off in your palm.
Here’s a myth I hear all the time: tempering is a “one and done” step. Nope, it’s a game of adjustments, and small tweaks make huge differences. If I have a customer making small fasteners that need to bend a little without breaking, I’ll tell the steel mill to hold the temper at 850°F for an extra hour. That extra soak time lets the carbon particles rearrange even more, so the steel is a little less brittle. If they’re making a heavy-duty pin for construction equipment that takes constant impact, I’ll nudge the temper temp down 50°F—harder, a touch less flexible, but way better at withstanding repeated bangs. I also make sure to mention this to every new customer I work with, because ordering “carbon steel” isn’t one-size-fits-all—tempering is part of that customization.
Another thing I see mix-ups about: tempering vs. annealing. Annealing is another heat treatment we do, but that’s for making steel super soft so you can machine it easily before it’s formed into a part. For example, if someone’s making a custom machine part that needs to be drilled and shaped in a lathe first, we anneal the raw steel so it’s soft enough to cut. Then once it’s shaped, we quench and temper it to get it hard and tough again. Tempering is always the last step before finishing, right before it ships to the customer. That’s a key difference, and I’ve had more than one new guy order annealed steel when they actually needed tempered—oops, that’s a quick lesson we fix fast.
Wait, let’s talk about stress relief too, because that’s related to tempering and something I actually do for some of my thicker steel plate products. When you make a big steel plate—like 4 inches thick for construction beams—quenching a thick piece causes uneven cooling: the outside cools fast, the inside cools slow. That leaves hidden internal stress, so if you cut a big beam out of that plate, it might warp or even crack weeks later when it’s on a job site. So we do a low-temperature temper (around 400–500°F) called stress tempering. It doesn’t harden the steel much, but it releases all that hidden stress, so the beam stays straight after cutting, and doesn’t crack when you weld it to other parts. Super important for big construction projects, and I make sure all my construction-grade steel gets that step.
Now, for the science nerds out there (yes, I know a lot of my regular customers are hands-on engineers, so I’ve picked up some of this): martensite, the structure we get from quenching, is actually metastable. That means it wants to rearrange into a more stable structure (called tempered martensite) when you heat it. The lower the temper temp, the less the rearrangement—so more martensite left, harder steel. The higher the temp, the more we turn martensite into soft, ductile ferrite and tiny carbide particles mixed in. Those carbides are key—they act like little barriers that stop cracks from spreading, which is why tempered steel is tough, not just hard. That’s the sciencey bit that makes all the real-world stuff work, and it’s why I don’t cut corners on tempering: bad tempering = steel that fails, and no one wants their bolt snapping on a highway or their drill bit breaking mid-job.
I’ve had a few horror stories over the years about what happens when tempering is done wrong. Last year, a small manufacturing client ordered some 1095 carbon steel from a competitor, tried to make knives with it, and the knives snapped in half when someone used them to cut cardboard (weird, I know, but it happened). Turned out the competitor skipped tempering entirely, or did a super fast temper at too low a temp, leaving it all brittle martensite. I helped them rework their knives with steel from me that got a proper temper at 750°F, and now their knives are some of the best-selling ones on Amazon. That’s the stuff that makes me love my job—knowing that the step I take seriously every day makes a real difference for people’s work.
Here’s the thing I want all my customers (and anyone reading this) to take away: tempering isn’t just a factory buzzword. It’s the reason the carbon steel I supply can be a soft, bendable sheet one week and a hard, impact-resistant part the next. It’s a balancing act: get the temp right, hold it for the right time, and you get steel that works exactly for what you need. Get it wrong, and you’ve got scrap, or worse, a product that fails when you need it most.

If you’re reading this because you need carbon steel for a project—whether it’s a custom part for a machine, heavy-duty construction materials, tools, or anything else—don’t hesitate to reach out. I’m here to walk you through exactly what tempering steps your steel needs, no confusing jargon, no hidden fine print. We can talk about what your part will be used for, how much flexibility it needs, how much impact it’ll take, and make sure we get the temper (and all the other steps) exactly right for you. Just send over the details on what you’re working on, and we can start figuring out the right carbon steel solution.
Pipe Reference:
- Callister, W. D., & Rethwisch, D. G. (2018). Materials Science and Engineering: An Introduction (10th ed.). Wiley.
- ASM International. (2020). Heat Treater’s Guide: Practices and Procedures for Irons and Steels (3rd ed.). ASM International.
- The Fabricator. (2021, August 12). “Understanding Carbon Steel Heat Treatment: Quenching, Tempering, and Annealing.” The Fabricator.
Wuxi Xuanyi Stainless Steel Co., Ltd.
Wuxi Xuanyi Stainless Steel Co., Ltd. is one of the most professional carbon steel manufacturers and suppliers in China. With abundant experience, we warmly welcome you to wholesale bulk durable carbon steel made in China here from our factory. If you have any enquiry about cooperation, please feel free to email us.
Address: Room 1207, Building 11, Shengang Metropolis Plaza, No. 299 Fangcheng Avenue, Xinwu District, Wuxi City,China.
E-mail: jscherryxy@163.com
WebSite: https://www.xuanyisteel.com/
