If you’ve ever stood next to an annealing furnace during a production shift, you know that one of the biggest hidden costs isn’t the material you’re heating—it’s the heat that slips out before it can do its job. As someone who’s spent the last 12 years building annealing furnaces for metal fabricators, automotive parts makers, and aerospace component suppliers, I’ve seen first-hand how companies lose 15 to 25 percent of their furnace heat to avoidable losses. Those numbers add up fast: for a mid-sized shop running a furnace 24/5, that can translate to $20,000 to $50,000 in wasted energy annually, not to mention the extra emissions that come with burning more fuel than necessary. The good news is, most of this loss isn’t inevitable. It boils down to small, consistent adjustments and targeted upgrades that work with a furnace’s design, not against it. Over the years, I’ve walked dozens of production floors with clients, tweaked their setups, and refined our furnace builds to cut that waste. Here’s what I’ve learned about reducing heat loss in annealing furnaces, with lessons I’ve picked up in real shops, not just textbook theory. Annealing Furnace
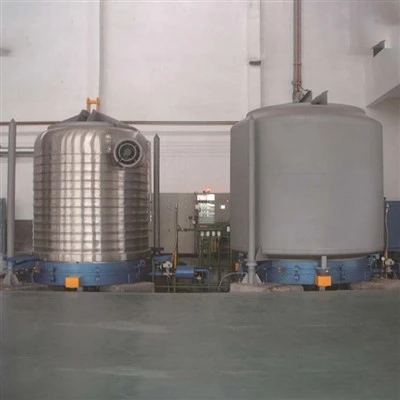
First, let’s start with the most common, and often the easiest to fix, source of heat loss: improper door and seal maintenance. This is the number one culprits I see on older furnaces. A 1/8-inch gap between a furnace door and its frame might not sound like much, but over a full week of operation, that gap can leak enough heat to warm a 10×10 room by 10 degrees Fahrenheit—enough to force the furnace’s heating elements to work overtime to maintain temperature. Most of the time, this loss comes down to worn seals or doors that aren’t aligned correctly after years of heavy use. On our newer furnaces, we use a graphite-impregnated silicone seal that stays flexible and air-tight even at annealing temperatures (which typically hover between 1,200 and 1,800 degrees Fahrenheit, depending on the metal being treated). But even these seals need upkeep. I once worked with a steel tubing shop that thought their seal issue was a bad heating element, until we checked the door: a small piece of debris (a metal shaving, in this case) had gotten wedged between the door and frame during a load change, leaving a gap they’d missed during their daily checks. That one gap was costing them $7,000 a year in wasted natural gas. The fix was simple: a 5-minute check before each shift to wipe the door frame and test for a tight seal by holding a piece of paper between the door and frame—if it slips out easily, the seal needs adjustment or replacement. For older furnaces that can’t be retrofitted with our custom seals, I recommend replacing standard fiber seals with ceramic fiber gaskets, which are more durable at high temperatures and create a tighter seal than the old rope-style seals many shops still use. I also suggest checking door alignment every three months, since heavy load movement can shift the frame slightly over time.
Next, heat loss through the furnace walls and ceiling—often called conductive loss—is another big source, particularly for furnaces that are 10 years or older. Annealing furnaces are lined with insulating materials to keep heat inside, but over time, that insulation can break down from repeated heating and cooling, or from being bumped by heavy metal loads during loading and unloading. On our new furnaces, we use a two-layer insulation system: a dense firebrick inner layer that directly faces the heat, and a lightweight, high-temperature ceramic fiber outer layer that traps heat and prevents it from seeping through the steel outer shell. This dual layer cuts conductive loss by 20 to 25 percent compared to single-layer insulation. But if you have an older furnace, you don’t have to replace the entire lining to see gains. Small repairs go a long way: patching small cracks in the insulation with high-temperature refractory cement, or replacing worn-out sections of ceramic fiber every 5 to 7 years. I recently had a client with a 15-year-old furnace that was losing 18 percent of its heat through the walls; after patching 6 small cracks and replacing a 2-foot section of lining near the loading door, we brought that loss down to 10 percent. It’s worth noting that not all insulation upgrades are worth the cost. Adding a thicker outer layer to an already well-insulated furnace can give you diminishing returns—most conductive loss is fixed by addressing gaps or damaged sections, not just piling on more material.
Another often-overlooked source of heat loss is the opening and closing of the furnace door during load changes. Every time that door swings open, hot air rushes out, and cold air pulls in from the production floor—this is called infiltration loss, and it can account for 10 to 15 percent of total heat loss in a furnace that’s loaded multiple times a day. I’ve seen shops with operators who rush through load changes, leaving the door open for 3 or 4 minutes at a time, just to get the next batch in. That’s a mistake. The fix here isn’t slowing down production—it’s automating load changes where you can. On our furnaces, we offer pneumatic door systems that open and close in less than 10 seconds, compared to 30 to 45 seconds for manual doors. For shops that can’t upgrade to our automated doors right away, we suggest setting clear expectations for load change times: train operators to limit door openings to the exact time needed to slide a load in or out, and use a light timer near the door to remind them when it’s been open too long. One automotive parts shop I work with did this, and cut their average door open time from 2.5 minutes to 45 seconds per load, saving them $12,000 a year in energy costs. Another trick I’ve used with clients is installing small, secondary access doors for temperature probes or sensor checks, instead of opening the main door every time you need to adjust a reading. That cuts down on unnecessary main door openings, which is a win for both heat retention and operator safety.
Now, let’s talk about something that’s less intuitive but just as important: flue gas loss. Every annealing furnace burns fuel (natural gas, propane, or electricity) to heat its interior, and the exhaust gases that come out of the flue carry a lot of unused heat with them. On many older furnaces, flue gases exit at temperatures of 500 to 700 degrees Fahrenheit—wasting heat that could be used to preheat either the incoming air for combustion or the incoming metal loads. We’ve designed our newer furnaces with a heat recovery system that captures that waste heat from the flue and uses it to preheat the combustion air before it enters the furnace. This cuts flue gas loss by 18 to 22 percent, depending on the furnace’s size. For example, a furnace with a 6-foot flue that was exhausting gas at 650 degrees can have that gas cooled to 250 degrees by the heat recovery system, with the captured heat being used to warm air that’s mixed with fuel before combustion. It sounds complicated, but it’s not—we’ve installed these systems on furnaces as small as 1,000 cubic feet, and the payback period is usually less than two years. For shops that aren’t ready for a full heat recovery system, a simpler fix is trimming the flue opening to the right size. I’ve seen furnaces with flues that are too large for their output, which lets more hot gas escape than necessary. A properly sized flue is just big enough to let exhaust gases out without pulling excess air into the furnace, which is another source of heat loss.
One more area I see companies miss is load management inside the furnace. A lot of operators will leave empty space in the furnace chamber to avoid stacking loads too tightly, or underload the furnace because it’s easier to handle smaller batches. But that empty space means there’s less material to absorb and retain heat, so more heat escapes through the walls when the door is open. The goal is to load the furnace to at least 70 to 80 percent of its rated capacity every time you run a batch. I worked with a small metal forging shop that was running half loads 80 percent of the time, because their dies were only made for small batches. We worked with them to adjust their load racks so they could fit two smaller batches back-to-back, instead of one, and by running full loads every time, they cut their total heat loss by 12 percent. It’s also important to arrange loads evenly inside the chamber, not just stacked haphazardly. If you pile heavy, dense loads on one side of the furnace, that side will hold heat differently than the other, leading to hot spots that force the furnace to cycle its heating elements more often, wasting energy.
I’ll be straight with you: none of these fixes will pay for themselves overnight. But the cumulative savings add up fast, especially when you pair small, low-cost adjustments (like seal checks or load time training) with targeted equipment upgrades that make sense for your furnace’s age and production needs. As an annealing furnace supplier, I don’t push every client to replace their entire furnace at the first sign of heat loss. Most of the time, a $500 seal replacement and a few hours of operator training will give them 80 percent of the savings they’d get from a new furnace. But when a client is ready for an upgrade, our dual-layer insulation, fast-door systems, and heat recovery units are designed specifically to cut that avoidable heat loss from day one. If you’re tired of watching energy bills climb, or you’re not sure where your furnace is losing the most heat, I’d be happy to walk through your setup with you, no sales pitch required. We can do a simple heat loss audit (we’ve got a portable thermal camera that spots gaps in insulation or worn seals in 15 minutes) and outline exactly what changes will give you the biggest return for your budget. Whether you need to tweak your current setup or look at a new furnace that’s built for efficiency, that’s what we’re here for.
It’s important to remember that reducing heat loss isn’t just about saving money on energy. Every unit of gas or electricity you don’t burn means less carbon emissions, too—for shops that work with automotive or aerospace clients, which often have strict sustainability targets, those savings add up on that front as well. I’ve seen clients turn those energy savings into extra revenue by bidding on jobs that require low-emission production, or by plowing the savings back into new equipment or raises for their teams. At the end of the day, annealing is all about getting consistent, high-quality results from your metal, and heat loss doesn’t just hurt your bottom line—it can hurt your parts, too. If the furnace is working overtime to make up for lost heat, you might see inconsistent hardness or grain structure in your parts, which can lead to rejects. That’s another cost most shops don’t account for.
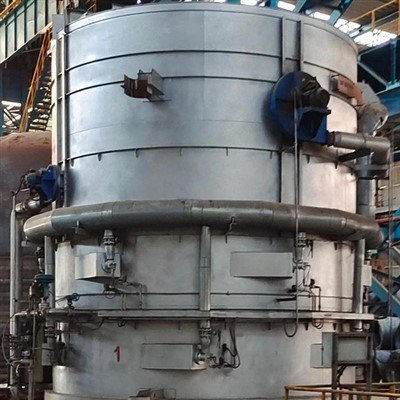
If you’re ready to take a closer look at your annealing furnace’s heat loss, or you have questions about what changes will work best for your operation, don’t hesitate to reach out for a no-obligation consultation. We work with small job shops and large manufacturing facilities alike, and we tailor every recommendation to your specific needs, not a one-size-fits-all sales pitch. Let’s talk about how we can cut your waste, boost your efficiency, and keep your annealing parts consistent and on-spec.
Crucible Furnace References
- ASM International. (2005). Heat Treater’s Guide: Practices and Procedures for Iron and Steels. ASM International.
- Gupta, S. (2017). Industrial Furnaces: Design, Applications, and Energy Efficiency. CRC Press.
- American Iron and Steel Institute. (2020). Energy Efficiency Guidelines for Heat Treatment Furnaces. AISI Publication.
- Haldar, A., & Suwas, S. (2011). Microstructure and Properties of Alloy Steels. Springer.
- Energy Star. (2019). Industrial Furnaces and Boilers: Energy Efficiency Opportunities. U.S. Environmental Protection Agency.
Danyang Dingfeng Industrial Furnace Co., Ltd.
Danyang Dingfeng Industrial Furnace Co., Ltd. is one of the most experienced annealing furnace manufacturers and suppliers in China, also supports customized service with low price. Please feel free to wholesale high quality annealing furnace made in China here from our factory. For pricelist, contact us now.
Address: Lizhuang Economic Development Zone, Danyang City
E-mail: saleszk@dffurnace.com
WebSite: https://www.dffurnace.com/
